Injection Mold Maintenance Checklist:Preventive Maintenance, Cleaning and Inspection Guide
2026-10-16 10:49:51
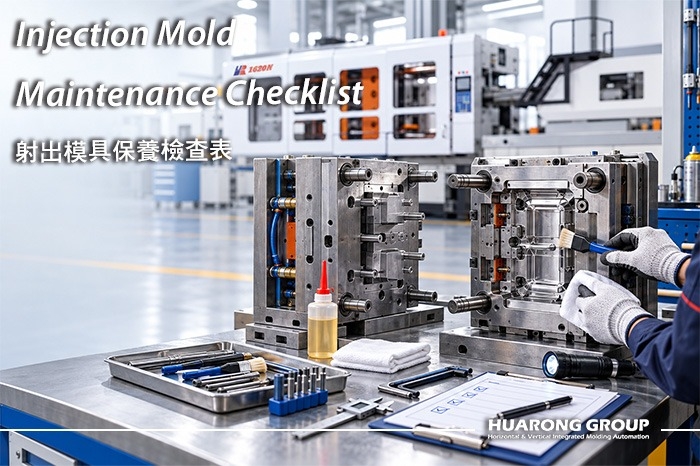
Injection mold maintenance involves inspecting, cleaning, lubricating, and protecting mold components to prevent premature wear, molding defects, and unplanned downtime. A practical plastic injection mold maintenance checklist should cover cavity and core surfaces, parting lines, vents, ejectors, slides, cooling channels, and moving mechanisms.
Maintenance frequency depends on the mold design, resin type, production cycles and operating conditions. This guide explains what to inspect, how to perform preventive maintenance, and when to pay extra attention.
Not every mold requires the same maintenance procedure. A simple two-plate mold has different inspection needs from a multi-cavity mold equipped with hydraulic cores or a hot runner system.
This injection mold maintenance checklist organizes the main inspection points by maintenance stage.
| Inspection Area | Routine Inspection | Preventive Maintenance | Before Storage |
| Cavity and Core | Resin residue, scratches, corrosion | Detailed cleaning and surface inspection | Clean and apply approved rust protection |
| Parting Line | Flash, contamination, damaged edges | Inspect wear and shut-off surfaces | Clean and protect |
| Mold Venting | Deposits, blockage, burn marks | Clean vents and inspect for damage | Remove deposits |
| Gate and Runner | Blockage, gate damage, abnormal wear | Inspect and clean accessible areas | Remove residual material where applicable |
| Ejector System | Smooth movement, complete return | Inspect pins, guides and lubrication | Position and protect as specified |
| Slides and Core Mechanisms | Movement, position confirmation | Inspect wear, alignment and lubrication | Clean, lubricate and secure |
| Cooling Channels | Leakage, flow and temperature stability | Inspect scale, corrosion and restrictions | Drain or protect as specified |
| Guides and Fasteners | Abnormal movement, loose components | Inspect wear and secure fasteners | Protect exposed surfaces |
| Sensors and Connections | Damaged wiring, abnormal signals | Verify position signals and connections | Protect connectors |
For molds with hot runners, valve gates, or specialized mechanisms, additional inspections must follow the relevant manufacturer's instructions.

A maintenance checklist identifies what needs attention. The next step is to carry out the work safely and consistently.
Before maintenance, identify the mold, resin grade, cumulative shot count, and any recent production problems.
Follow the applicable machine, such as injection molding machine shutdown and hazardous energy control procedures. Electrical power, stored hydraulic or pneumatic pressure, residual heat, and unexpected mechanical movement may present hazards.
Where servicing exposes personnel to hazardous energy, use the required lockout/tagout procedures. Normal machine safety interlocks are not a substitute for proper energy isolation.
Remove resin residue, deposits, and contamination from accessible cavity, core, parting, and vent surfaces.
Cleaning methods should be compatible with the mold steel, surface coating, finish, and processed resin. Use approved non-damaging tools and cleaning products.
Avoid abrasive cleaning that could change precision surfaces. Mold vents must retain their designed dimensions, so clean blocked vents rather than enlarging them without engineering approval.

Check moving components for wear, contamination, misalignment, or insufficient lubrication.
For ejectors, verify smooth operation and complete return. For slides and core mechanisms, inspect guide surfaces, locking components, and position confirmation devices.
Mechanical movement and machine control must work together. A core that moves correctly but does not provide reliable position feedback can still interrupt the molding cycle.
For complex molds, verify the approved movement sequence and related interlocks before production.
Further reading:Core Pull Injection Molding: Engineering Guide.
Cooling channels are often overlooked because their internal condition is not directly visible.
Scale, corrosion, blockage, or leakage can reduce heat transfer and contribute to uneven mold temperatures, dimensional variation, and longer cooling times.
During maintenance, check:
- Cooling water leakage and connection condition
- Flow consistency in individual circuits
- Inlet and outlet temperatures against the established process baseline
- Signs of restrictions, deposits, or corrosion
If cooling performance declines, inspect both the mold circuits and the external temperature control equipment.
A stable chiller outlet temperature does not necessarily mean every mold circuit has sufficient flow.
Cleaning or flushing should follow an approved procedure compatible with the mold materials, seals, and cooling medium.
Further reading:Chiller for Injection Molding:Cooling Stability.

After maintenance, confirm that all components are correctly reassembled and that no tools or cleaning materials remain inside the mold.
Qualified personnel should verify relevant mechanical movements, sensors, interlocks, cooling connections, and mold protection settings before restarting production.
Inspect the initial molded parts for appearance and dimensional quality before returning the process to normal operation.
No universal shot count or fixed maintenance interval fits every injection mold.
Preventive mold maintenance should be based on the mold maker's recommendations and actual production conditions.
| Maintenance Level | When to Perform | Purpose |
| Routine Inspection | During production checks or changeover | Identify contamination, leakage, and abnormal operation |
| Scheduled Preventive Maintenance | At mold-specific intervals based on operating history | Detailed cleaning, lubrication, and component inspection |
| Major Inspection or Repair | When wear, recurring defects, or damage indicate a need | Evaluate and repair affected tooling components |
Maintenance intervals may need adjustment when processing abrasive materials such as glass-fiber-reinforced resins, using formulations that generate corrosive degradation products, or operating molds with complex moving mechanisms.
Rather than relying only on shot count, review maintenance records and recurring production problems to decide whether to change inspection frequency.
Changes in molded part quality can signal early tooling problems.
However, not every defect originates from the mold. Material condition, machine settings, and processing parameters should also be considered.
| Production Symptom | Possible Mold-Related Cause | What to Inspect |
| Increasing Flash | Parting line wear or contamination | Parting and shut-off surfaces |
| Burn Marks | Restricted mold venting | Vent entrances and exhaust paths |
| Short Shots | Vent blockage or gate restrictions | Vents, gates and runners |
| Part Sticking or Ejector Marks | Ejector wear, interference, or surface condition | Ejector system and molding surfaces |
| Warpage or Longer Cooling Time | Restricted or uneven cooling | Individual cooling circuits |
| Abnormal Slide Movement | Wear, poor lubrication, or misalignment | Slides, guides, locking surfaces and position feedback |
For example, if flash repeatedly appears in the same cavity location, inspect the corresponding parting and shut-off surfaces. If the defect changes with packing pressure or other processing adjustments, investigate both mold condition and process settings before deciding on corrective action.
Related troubleshooting guides:
Flash Injection Molding: Causes and Solutions
Burn Marks in Injection Molding: Causes and Prevention
A mold maintenance checklist is more useful when you document each inspection.
A maintenance record should identify the mold, resin grade, production shot count, inspection date, technician, component condition, and corrective actions.
Use the following status definitions:
- OK:The inspected item meets the applicable requirements.
- NG:An abnormality requires corrective action or review.
- N/A:The item does not apply to this mold.
Record significant findings, such as recurring vent deposits, worn ejector pins, or changes in cooling circuit performance.
These records provide a reference for future inspections and help maintenance teams distinguish repeated problems from new failures.
The checklist can be used as a reference for routine inspections, preventive maintenance, and mold storage preparation.
Before storing a mold, remove contamination, inspect critical surfaces, and apply approved corrosion protection.
Cooling circuits should be drained, dried, or otherwise protected according to the mold maker's instructions and storage conditions.
Position moving components correctly, protect fluid and electrical connections, and record the mold's maintenance status.
When reinstalling a stored mold, inspect its condition and verify the necessary mechanisms before production.
Premature wear may result from abrasive fillers, contamination, poor lubrication, misalignment, corrosion, or repeated mechanical interference. Identify the cause by inspecting components and reviewing operating history before repair or replacement.
Machine settings can influence defects such as flash, sticking, or dimensional variation, but they cannot repair damaged mold surfaces, worn components, or blocked cooling passages. Evaluate both the process and the mold condition.
Yes. Depending on its design, a hot runner system may require inspection of heaters, thermocouples, electrical connections, nozzles, and valve gate mechanisms. Follow the hot runner manufacturer's maintenance and safety procedures.
Mold maintenance focuses on the tooling that forms and ejects the plastic part. Machine maintenance covers the injection unit, clamping system, hydraulic and electrical systems, and machine controls.
For machine-specific procedures, see Huarong's Injection Molding Machine Maintenance PDF and Checklist.
Effective injection mold preventive maintenance combines regular inspection, appropriate cleaning, mechanical checks, cooling circuit monitoring, and documented results.
The goal is not simply to complete a checklist, but to identify developing problems and maintain consistent molding conditions.
If you are experiencing recurring injection molding defects, unstable cycle times, or unexpected machine operation, Huarong can help review the available process and equipment information.
Provide your part details, resin grade, mold type, machine model, defect photos, and current processing conditions to support a technical discussion about possible machine, mold operation, or process-related causes.
- Group Name: Huarong Group
- Brand: Huarong, Yuhdak, Nanrong
- Service Offerings: Injection Molding Machine, Vertical Injection Molding Machine, Injection Molding Automation
- Tel: +886-6-7956777
- Address: No.21-6, Zhongzhou, Chin An Vil., Xigang Dist., Tainan City 72351, Taiwan
- Official Website: https://www.huarong.com.tw/