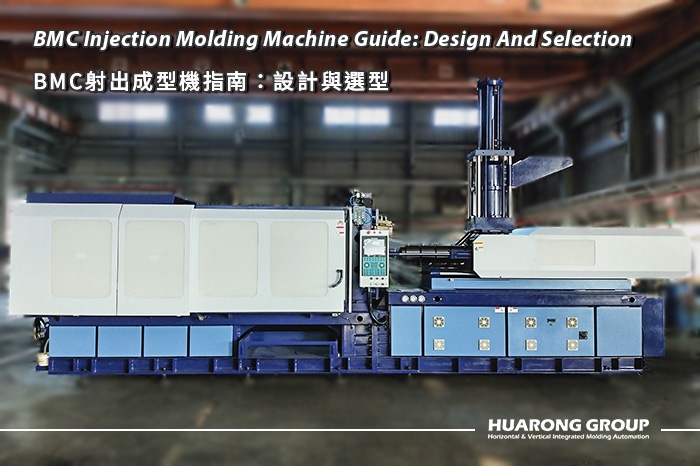
BMC Injection Molding Machine Guide: Design And Selection
2026-09-30 09:12:05
BMC, or Bulk Molding Compound, is a thermoset composite molding material widely used for electrical components, automotive parts, industrial components, and other applications that require dimensional stability, heat resistance, electrical insulation, and mechanical performance.
However, molding BMC is not simply a matter of processing a different type of plastic. BMC has distinct material characteristics that affect feeding, plasticizing, injection, mold temperature, curing, and equipment wear. These differences make machine configuration an important factor in achieving consistent production.
When evaluating a BMC injection molding machine, manufacturers should therefore consider more than clamping force and injection capacity. Material feeding, screw and barrel configuration, wear resistance, temperature control, mold requirements, shot repeatability, and automation can all influence long-term production performance.
Bulk Molding Compound (BMC) is a thermoset composite molding material typically consisting of a thermosetting resin, reinforcing fibers, mineral fillers, additives, and other formulation-specific components.
Unlike thermoplastics, which can generally be softened by heating and solidified again through cooling, BMC undergoes an irreversible curing reaction during molding. Heat activates the curing system, allowing the material to develop its final mechanical and thermal properties.
This behavior creates several equipment requirements. First, BMC must be delivered into the injection unit in a controlled and consistent manner. Its formulation may contain abrasive fillers and reinforcing fibers, which can increase wear on components that come into contact with the material. Second, the injection unit must be configured to process the specific BMC formulation without causing excessive material degradation or premature curing. Third, mold temperature plays a critical role because the mold provides the thermal conditions required for curing after the material has been injected.
For these reasons, a BMC injection molding machine is generally configured differently from a conventional thermoplastic injection molding machine.

Thermoplastic materials are commonly supplied as pellets and are softened by heat inside the barrel before injection. After filling the mold, the material is normally solidified by cooling.
BMC behaves differently. It is a thermoset compound containing resin, fillers, fibers, and other formulation components. The material must be handled and injected while maintaining the appropriate processing conditions before curing takes place in the mold.
The formulation can also affect viscosity, fiber behavior, wear, and flow characteristics.
For thermoplastics, barrel heating is primarily used to melt the material, while mold temperature is often associated with cooling, surface quality, crystallization, or cycle-time control depending on the resin.
For BMC, the relationship between temperature and curing is different.
The injection unit must maintain suitable conditions for material preparation and injection while avoiding unwanted curing before the material reaches the mold. The mold is then heated to provide the thermal conditions necessary for curing.
Conventional thermoplastic injection molding machines are commonly designed around pellet feeding systems.
BMC may require a dedicated feeding and material-handling arrangement because its physical form and formulation can differ significantly from standard thermoplastic pellets.
Consistent feeding is particularly important because variations in material delivery can affect shot weight, filling behavior, and production repeatability.
Fillers and reinforcing fibers used in BMC formulations can contribute to component wear.
The screw, barrel, nozzle, and other material-contact components should therefore be evaluated according to the abrasiveness and formulation of the material being processed.
A conventional pellet conveying system is designed around the physical characteristics of pelletized thermoplastics. BMC may require a different feeding approach depending on its formulation and supply form.
The objective is to transfer the material into the injection unit consistently while minimizing material disruption and maintaining a predictable supply.
Consistent material feeding directly affects shot repeatability.
If the amount of material entering the injection unit fluctuates, the resulting shot weight can vary. This can lead to differences in filling, part weight, dimensional consistency, and curing behavior.
For high-volume BMC production, automated feeding can reduce manual material handling and improve production continuity.
An automated system should be evaluated based on:
- BMC material characteristics
- Required feeding capacity
- Material storage and replenishment
- Production cycle
- Operator involvement
- Integration with the overall production line
A BMC screw should be selected according to the material's processing characteristics rather than simply using a standard thermoplastic screw.
The geometry should support consistent material preparation and injection while considering the formulation's fillers, fibers, viscosity, and curing behavior.
BMC formulations can contain mineral fillers and reinforcing fibers that contribute to abrasive wear.
For this reason, wear-resistant material-contact components can be important for maintaining long-term machine performance.
In addition to abrasion, the chemical characteristics of a particular formulation should be considered.
Resin systems, additives, fillers, and processing conditions may influence the material-contact environment.
Consistent shot weight is essential for stable BMC production.
Variations in material feeding, screw position, injection behavior, or component wear can influence the amount of material delivered for each cycle.

The injection unit should maintain conditions suitable for the specific BMC grade.
The objective is to support stable injection without unnecessarily accelerating the curing reaction before the material reaches the mold.
Unlike many conventional thermoplastic processes where cooling is central to solidification, BMC molding relies on heat in the mold to initiate and control curing.
The mold temperature therefore affects more than surface quality. It is directly related to the curing process and consequently to cycle time and part performance.
Premature curing inside the injection unit can cause serious production problems.
If the material begins curing before it is completely injected, flow resistance may increase and material can accumulate in areas of the injection system.
BMC processing requires a balance between allowing the material to flow into the mold and providing sufficient heat for curing.
The optimal balance depends on the material formulation, part geometry, mold design, injection conditions, and target cycle.

The mold must provide the thermal conditions required for curing.
Temperature uniformity across the mold can become particularly important for multi-cavity tools or parts with significant differences in geometry and material flow.
BMC molding can generate gases during the curing process. Effective venting helps allow gases to escape from the cavity during filling and curing.
Insufficient venting can contribute to defects such as incomplete filling, surface marks, burns, or other molding problems.
Flash can result from factors including excessive injection pressure, insufficient mold clamping, parting-line conditions, mold wear, or process instability.
After curing, the part must be released from the mold without damaging critical features.
Ejection force and ejection timing depend on part geometry, material behavior, mold surface, and curing conditions.
Part weight is one of the first parameters to establish.
The required shot should account for the total molded material per cycle, including the parts and any relevant runner or process material.
Mold dimensions determine whether the tool can physically fit within the machine's platen and tie-bar area.
Clamping force must also be sufficient to resist mold-opening forces during injection and curing.
Different BMC formulations can have different flow characteristics, filler content, reinforcing fibers, curing systems, and processing requirements.
The BMC grade should therefore be confirmed before finalizing the machine configuration.
Cavity count directly affects production output.
A multi-cavity mold may increase output per cycle but can also increase requirements for filling balance, mold temperature uniformity, venting, and automation.
Automation may include material feeding, part removal, conveyors, inspection, counting, packaging, or other downstream operations.
Production stability should be evaluated over extended operating periods.
Key considerations include:
- Shot repeatability
- Material feeding consistency
- Component wear
- Temperature stability
- Mold temperature uniformity
- Cycle repeatability
- Maintenance requirements
- Automation integration
BMC typically combines thermosetting resin with fillers and reinforcing fibers, while Bakelite generally refers to phenolic-based thermosetting materials.
The physical form and handling requirements of BMC may differ from those of phenolic molding materials.
Both materials can require specialized screw, barrel, temperature control, and wear-resistant configurations.
However, the appropriate machine should be determined by the specific formulation rather than by the broad material category alone.
Before selecting a machine for either BMC or Bakelite production, manufacturers should confirm:
1. What is the exact material grade?
2. What is the material formulation and filler content?
3. What is the required part weight?
4. What is the mold size?
5. How many cavities are required?
6. What cycle time is targeted?
7. What feeding method is required?
8. What level of automation is needed?
9. What wear protection is recommended?
10. What mold temperature and curing conditions are specified by the material supplier?
Possible machine-side factors include inconsistent material feeding, screw or barrel wear, unstable injection conditions, or incorrect injection-unit configuration.
Poor filling may be associated with material flow characteristics, injection conditions, mold temperature, venting, or mold design.
Flash may be related to excessive pressure, insufficient clamping force, mold condition, parting-line wear, or process instability.
Premature curing can occur when material conditions inside the injection system allow the curing reaction to begin too early.
Accelerated wear may be associated with abrasive fillers or reinforcing fibers in the BMC formulation.
A BMC production project should be evaluated as a complete molding system rather than simply as a machine purchase.
For example, consider a production application requiring a multi-cavity BMC component with a defined part weight and target cycle.
The machine evaluation would begin with the BMC grade and its processing requirements. The part weight and cavity count would then be used to estimate the required shot capacity and production output.
Next, mold dimensions and projected area would be reviewed to determine the appropriate clamping capacity.
The material feeding system, screw and barrel configuration, and wear-resistant components would then be selected according to the BMC formulation.
Finally, mold temperature control, venting, part removal, and automation requirements would be integrated into the production cell.
A BMC injection molding machine is an injection molding system configured to process Bulk Molding Compound, a thermoset composite material.
It depends on the material, machine configuration, and production requirements.
BMC is a thermoset composite that commonly incorporates resin, fillers, and reinforcing fibers, while Bakelite generally refers to phenolic thermosetting material.
BMC formulations can contain abrasive fillers and reinforcing fibers, which may increase wear on material-contact components.
BMC feeding depends on the material's physical form and formulation. A dedicated feeding system may be used to provide consistent material delivery to the injection unit.
Shot size should be based on the total material required per molding cycle, including the molded parts and applicable process material.
Abrasive fillers and reinforcing fibers in some BMC formulations can accelerate wear.
- Group Name: Huarong Group
- Brand: Huarong, Yuhdak, Nanrong
- Service Offerings: Injection Molding Machine, Vertical Injection Molding Machine, Injection Molding Automation
- Tel: +886-6-7956777
- Address: No.21-6, Zhongzhou, Chin An Vil., Xigang Dist., Tainan City 72351, Taiwan
- Official Website: https://www.huarong.com.tw/